 Eileen Yu, Vice General Manager
Published Updated 2 min readTechnology
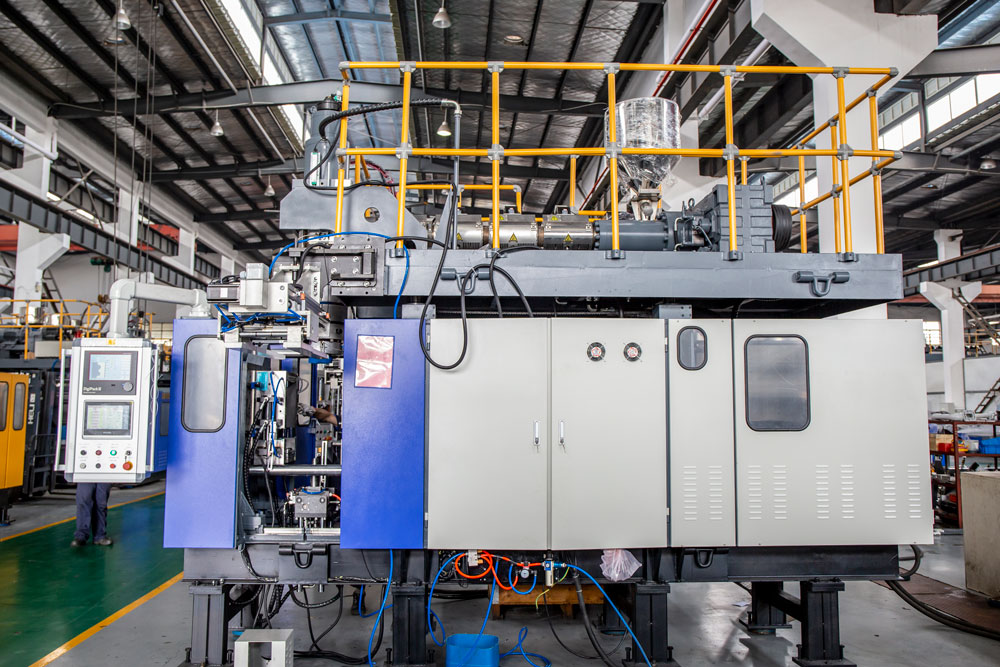
An extrusion blow molding machine designed to produce containers with a volume of more than 20 L is generally classified as a large extrusion blow molding machine. It is generally used for ultra-high-molecular-weight polyethylene (UHMWPE). Adapting to specific plastic processing characteristics, increasing blowing pressure, and using low-temperature, dry, high-pressure air are key to shortening cooling time and improving product quality. Shortening the production cycle and improving production efficiency is an important part of technological progress in large extrusion blow molding machines. Improving plasticizing capacity is a prerequisite for increasing production efficiency.
Improving accumulator head performance requires a high-performance flow path with a double-layered, heart-shaped envelope. First-in-first-out flow, quick color changes and easy cleaning are important features of a high-performance accumulator head. Development combines advanced CAD and CAE methods with high-quality steel and precision processing equipment.
In addition, the plug-type tie-barless clamping mechanism is a clamping structure developed in recent years, which has the characteristics of large clamping force and uniform distribution, easy loading and unloading of the mold, large capacity modulus, and energy saving. The guiding motion should adopt the ball linear guide with small friction coefficient, smooth motion and high running precision; the fast shifting is realized by the servo motor through the ball screw; the high-pressure clamping is the locking sleeve of one template inserted into the other template. After that, two or more pairs of clamping cylinders distributed on the left and right sides of one template are tensioned by another template, and vice versa.
The hydraulic synchronous tie-bar-less clamping mechanism utilizes two sets of symmetrical hydraulic drives to move the respective platens synchronously. Since the center of the template is driven by the driving cylinder, the weight of the template can be reduced, the amount of locking deformation can be reduced, and the mold can be loaded and unloaded. It is easier, more capacitive, and more suitable for the operation of the robot. It is superior to the plug-type tie-bar clamping mechanism in performance, and it is worthy of popularization and application.
The development and application of the Radial Wall Thickness Distribution System (PWDS), which works in conjunction with the axial wall thickness distribution system (AWDS), provides optimum draft and better product wall thickness distribution.